
2507 (UNS S32750, EN 1.4410, F53) is the super duplex grade that sits one step above 2205 and two steps below the 6% molybdenum austenitics. Its PREN of 42 or higher and 550 MPa minimum yield let a subsea flowline carry the same design pressure at roughly half the wall thickness of 316L — which is why the grade dominates seawater and sour service piping where weight and corrosion allowance both matter.
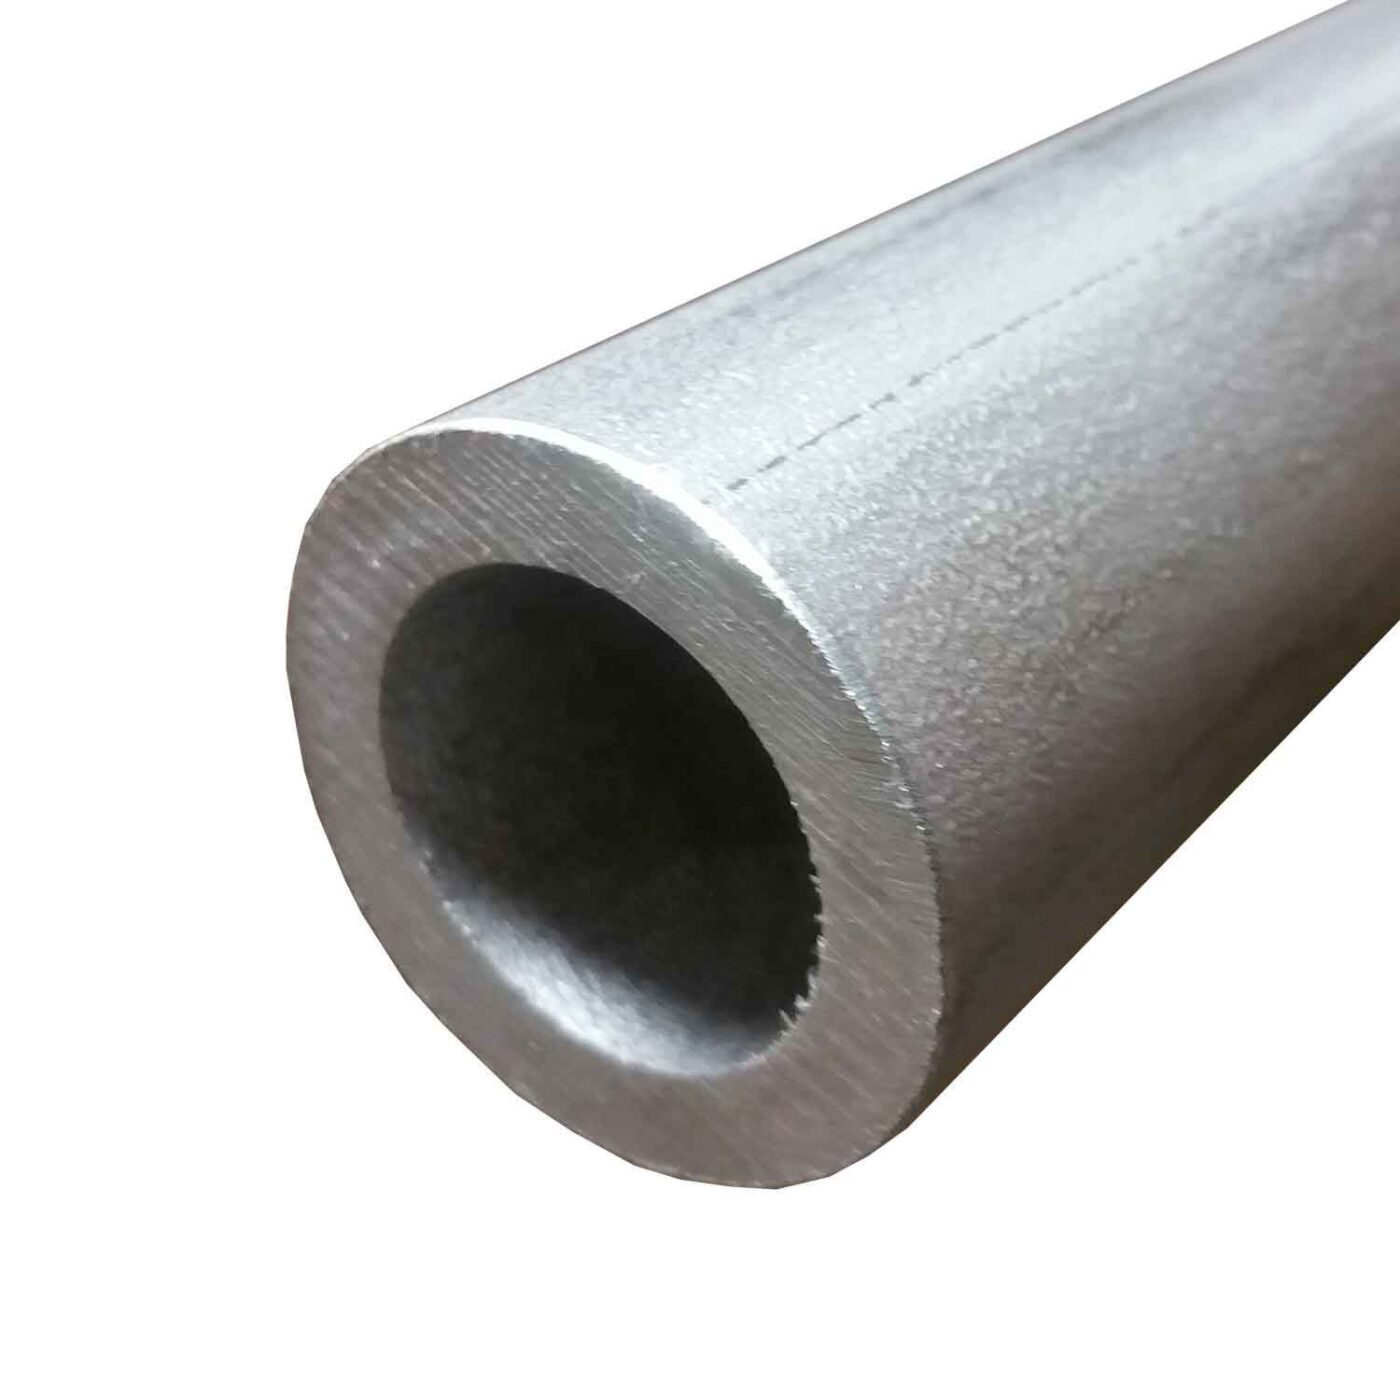
The chemistry is a 25% chromium, 4% molybdenum, 7% nickel balance with 0.24–0.32% nitrogen. The nitrogen is what makes the grade work: it stabilises austenite so the weld heat-affected zone re-forms a balanced 50/50 microstructure instead of turning into ferrite, and it lifts both yield strength and pitting resistance. That is the practical difference between 2507 and a lean duplex such as 2101, which relies on manganese and cannot match the corrosion resistance.
Compared with 2205, the step up is real but not free. PREN rises from about 34 to 42+, critical pitting temperature in ferric chloride moves from roughly 50 °C to above 80 °C, and yield strength rises from 450 to 550 MPa. The cost is tighter welding windows, lower toughness at sub-zero temperatures, and a 32 HRC ceiling in sour service — all of which must be designed for rather than discovered on site.
In oil and gas, 2507 pipe is specified for subsea flowlines and jumpers, seawater cooling and injection lines, topside process piping on FPSOs, and sour gas gathering where 2205 has insufficient pitting margin. Above roughly 90 °C in sour service the grade gives way to Alloy 2550 or a nickel alloy, so the operating envelope must be checked against NACE MR0175 rather than assumed.
2507 Pipe Standards and Equivalent Grades
Pipe is specified under ASTM A790 for seamless and welded product, A928 for welded pipe with filler metal, and A789 for tubing. The forging grade is A182 F53 and the bar grade is A479 / A276. Quoting A790 when the mill supplies A928 welded pipe is a specification mismatch that shows up at the witness test, so the manufacturing route has to be fixed before the order is placed.
We supply both routes: seamless pipe for critical subsea and sour service, and welded pipe for larger diameters where the seam is 100% radiographed and the weld is solution annealed inline.
| System | Designation |
| UNS | S32750 |
| W.Nr. / EN | 1.4410 / X2CrNiMoN25-7-4 |
| ASTM A790 | Seamless and welded pipe |
| ASTM A928 | Welded pipe with filler metal |
| ASTM A789 | Seamless and welded tube |
| ASTM A182 F53 | Forging and flange |
| NORSOK M-630 | MDS D55 / D57 |
Where 2507 Pipe Is Used
Subsea flowlines and jumpers
Production and water injection lines between templates and manifolds, where wall thickness drives weight and installation cost.
Seawater cooling systems
Heat exchanger tube bundles and cooling water headers on FPSOs and LNG plants, resistant to chlorinated seawater at 40 °C.
Sour gas gathering lines
Wet gas lines with H2S and chlorides, specified to NACE MR0175 at a 32 HRC maximum.
Topside process piping
High-pressure separator outlets and produced water lines where 2205 would need a corrosion allowance that the weight budget cannot absorb.
Desalination and water treatment
Brine lines and high-pressure membrane housings, where chloride concentration reaches 70,000 ppm.
Flare and vent lines
Wet flare headers exposed to alternating wet and dry conditions, prone to chloride concentration under deposits.
Supply Range and Delivery Condition
Seamless pipe from 6 mm to 610 mm outside diameter, wall 1.0 mm to 30 mm; welded pipe from 219 mm to 1,200 mm. Standard delivery is solution annealed at 1,025–1,125 °C with water quenching, pickled and passivated, in 6 m random lengths or cut to order.
Seamless pipe is supplied to A790 with the ordered wall thickness and either 1.25% or 2.5% tolerance — state which, because pressure design in this grade is sensitive to wall loss. Welded pipe is supplied with 100% radiography of the longitudinal seam and, on request, of the circumferential welds.
Testing includes hydrostatic test, eddy current or ultrasonic inspection, ferrite content by magnetic method or metallography (target 35–55%), ASTM A923 Method A and Method C for intermetallic phases, and ASTM G48 Method A pitting test at 40 °C or 50 °C depending on the purchase specification. Mill test reports to EN 10204 3.1 with heat traceability.
Chemical Composition of 2507 (wt%)
Nitrogen at 0.24–0.32% is the element to watch. Below 0.24% the weld zone loses austenite and the pitting resistance collapses; above 0.32% the ingot becomes prone to porosity. Every heat is checked by inert gas fusion rather than by difference.
Molybdenum at 3.0–5.0% is a wide range and sits at the centre of the commercial negotiation — a heat at 3.2% and a heat at 4.8% both meet the specification but deliver different PREN. We calculate PREN from the actual heat analysis and report it on the certificate.
| Element | Min % | Max % |
| Chromium (Cr) | 24.00 | 26.00 |
| Nickel (Ni) | 6.00 | 8.00 |
| Molybdenum (Mo) | 3.00 | 5.00 |
| Nitrogen (N) | 0.24 | 0.32 |
| Carbon (C) | — | 0.030 |
| Manganese (Mn) | — | 1.20 |
| Silicon (Si) | — | 0.80 |
| Copper (Cu) | — | 0.50 |
| Phosphorus (P) | — | 0.035 |
| Sulphur (S) | — | 0.020 |
| Iron (Fe) | balance | balance |
Mechanical Properties of 2507 Pipe
Values are the ASTM A790 minima for solution-annealed pipe at room temperature. The grade is not strengthened by heat treatment after the solution anneal; any further thermal cycle above 600 °C risks sigma phase and must be avoided or followed by a full re-anneal.
For sour service, NACE MR0175 caps hardness at 32 HRC (roughly 302 HB). Because the solution-annealed condition typically lands at 250–290 HB, the limit is normally satisfied without special processing — but it must be verified on the finished pipe, not on the billet.
| Property (room temperature) | ASTM A790 minimum |
| Tensile strength | ≥ 800 MPa |
| Yield strength (0.2%) | ≥ 550 MPa |
| Elongation in 50 mm | ≥ 15% |
| Hardness (NACE limit) | ≤ 32 HRC |
Need 2507 super duplex pipe to A790 or A928?
Send the outside diameter, wall thickness, quantity, seamless or welded route, and any NACE, G48 or A923 requirement — we reply with mill availability, lead time and a priced offer, usually within one working day.